Hard Anodized Aluminum Motorcycle Shock Absorber Parts
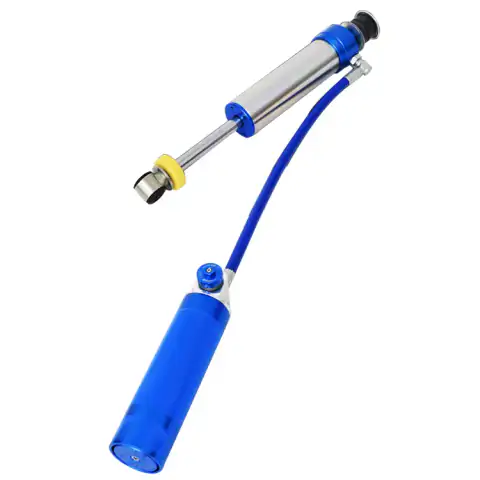
These are shock absorber components for motorcycles and cars, machined from aluminum and finished with Type III hard anodizing. Typical parts include reservoirs, preload adjusters, top caps, clevises and damper bodies. Hard anodizing gives a wear-resistant, corrosion-resistant surface that suits moving and threaded parts. They suit suspension brands and aftermarket shops building or upgrading shocks.
- Material
- Aluminum
- Tolerance
- to ±0.005 mm
- MOQ
- 1 piece
- Prototype lead time
- 3–7 days
- Type III hard anodizing, typically 25–50 µm
- Threads sized to run smoothly after coating
- Chamfered edges to prevent coating chips
- Steel, brass and copper parts machined alongside
Item ref. 60821833853 ·
| Process | CNC turning, CNC milling, Type III hard anodizing |
|---|---|
| Materials | Aluminum 6061-T6, 7075-T6; stainless steel, carbon steel, brass, copper |
| Surface Finish | Hard anodizing (natural, gray, black), plating, passivation |
| Tolerance | ±0.05 mm standard; down to ±0.005 mm on critical features |
| MOQ | 1 piece; prototypes through mid-volume runs |
| Drawing Formats | STEP, IGES, X_T, STL, DWG, DXF, PDF |
| Lead Time | Prototypes typically 3–7 working days; production usually 10–20 |
| Inspection | FAI, in-process checks, 100% critical dimensions; CMM |
Manufacturing
How we make this part
Process, material options and inspection for hard anodized aluminum motorcycle shock absorber parts.
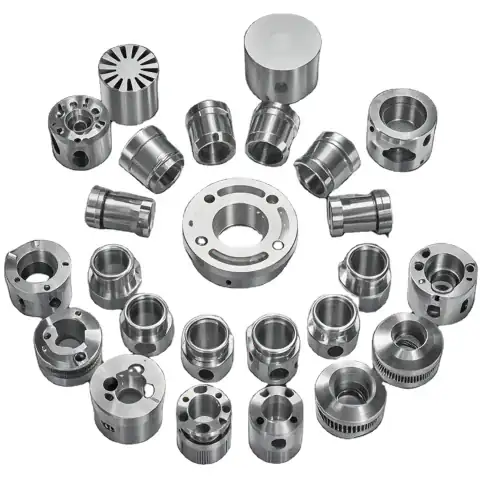
Parts are turned and milled from 6061 or 7075 bar. Threads for preload collars are cut with precise pitch and depth so the adjuster spins smoothly after anodizing. Clevis eyes are bored for bearings or bushings, and reservoir mounts are milled with clamp slots. Sharp edges are chamfered before hard anodizing, because the coating can chip on sharp corners.
Type III hard anodizing builds a coating typically 25–50 µm thick, about half penetrating the surface and half building up, with hardness far above the base aluminum. It is usually natural gray, dark gray or black; bright colors are limited. Steel, stainless, brass and copper components in the shock are machined separately and finished with plating or passivation.
Thread fit after anodizing, bore sizes and coating thickness are checked on samples from each batch. Visual inspection checks for burns and uneven coating. Common products are motorcycle rear shock preload collars, reservoir caps, front fork caps, damper adjuster knobs, clevis ends and shock bodies for street, track and off-road motorcycles.
FAQ
Frequently asked questions
What color can hard anodized shock parts be?
Hard anodizing is naturally gray to dark bronze depending on alloy and thickness, and it is commonly dyed black. Bright colors like red or blue are difficult because the thick coating is dark and dense. If bright colors matter, use Type II color anodizing on cosmetic parts and hard anodize only the wear surfaces.
How much does hard anodizing change thread fit?
A 50 µm hard coat grows about 25 µm outward per surface, which on threads affects pitch diameter noticeably. We adjust thread dimensions before coating or mask threads. Specify whether gauges must pass after anodizing so we plan the compensation correctly.
How do I get a quote for hard anodized aluminum motorcycle shock absorber parts?
Send a 3D model (STEP or IGES) and a 2D drawing with tolerances, material, finish and quantity through the quote form or by email. An engineer replies within 24 hours on business days with price, lead time and any DFM suggestions.
Request a quote
Quote this part
Attach drawings or send several parts at once from the full quote form.
- Emailinquiry@machined-parts-factory.com
- WhatsApp+86 176 2154 1688
- Phone+86 176 2154 1688
- HoursMon–Sat, 08:30–18:00 China Standard Time (UTC+8)