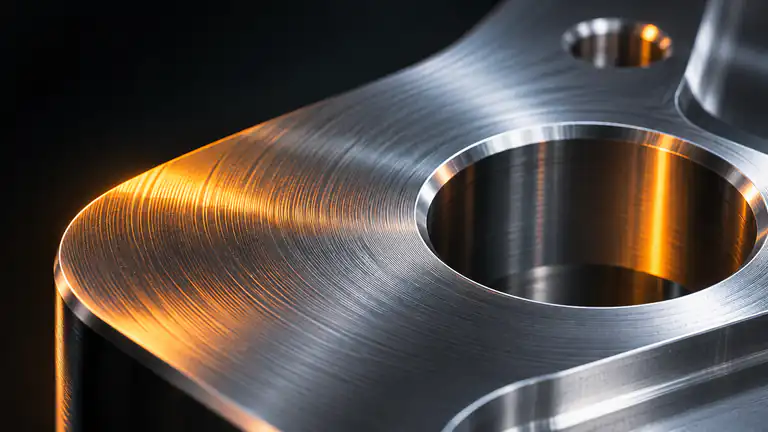
CNC Milled 7075 Aluminum Fixture Plate
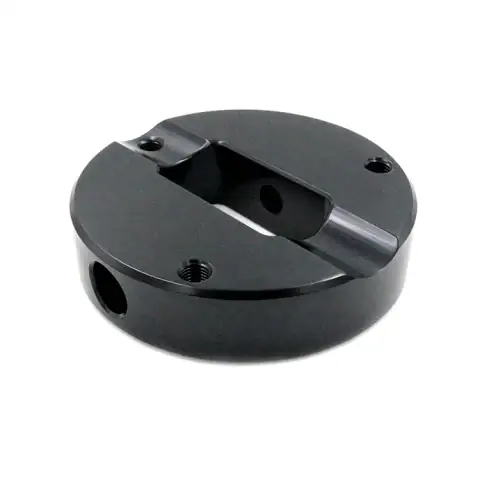
This is a custom fixture or tooling plate CNC milled from 7075-T6 or 6061-T6 aluminum, with dowel holes, tapped grids, pockets and locating features. Faces are machined flat and holes positioned to 0.01–0.05 mm, then the plate is anodized for wear and corrosion protection. It suits automation integrators, test-equipment builders and machine shops building fixtures and jigs.
- Material
- Aluminum
- Tolerance
- to ±0.005 mm
- MOQ
- 1 piece
- Prototype lead time
- 3–7 days
- Stress-relieved plate machined flat
- Reamed dowel holes for slip fits
- Type III hard anodize for wear faces
- CMM true-position report for locators
Item ref. 1600789705564 ·
| Process | 3-axis CNC milling, boring, reaming |
|---|---|
| Materials | Aluminum 7075-T6, 6061-T6 |
| Tolerance | 0.01–0.05 mm on dowel and locating holes |
| Surface Finish | Type II or Type III hard anodizing |
| MOQ | 1 piece |
| Drawing Formats | STEP, IGES, X_T, STL, DWG, DXF, PDF |
| Lead Time | Prototypes ~3–7 working days; production typically 10–20 working days |
| Inspection | First-article + 100% critical-dimension inspection; CMM report on request |
| Options | Press-fit steel dowel bushings, laser-engraved grid labels |
Manufacturing
How we make this part
Process, material options and inspection for cnc milled 7075 aluminum fixture plate.
Fixture plates must stay flat, so we start from stress-relieved plate, face both sides with alternating cuts and let the plate relax before final skimming. Dowel holes are bored or reamed for slip fits, and tapped hole grids are drilled with spot-drill control for true position. Large plates are clamped at the edges to avoid distortion. Where needed, the datum face is finished last.
7075-T6 is harder and more wear-resistant than 6061, so locating features last longer under repeated loading; it also costs more. 6061-T6 is the economical choice for plates where wear is light. Type III hard anodize, typically 25–75 µm, adds substantial surface hardness for fixture contact faces, while Type II is fine for general plates. Steel dowel bushings can be pressed in for heavy-use locations.
Flatness is checked on a granite surface plate and dowel hole positions on CMM. We report true position for locating features at first article. Plates are 100% inspected for critical dimensions and packed with protective film to avoid face scratches. Typical uses include machining fixtures, assembly jigs, test nests, robot tool plates and modular tooling bases.
FAQ
Frequently asked questions
How flat can an aluminum fixture plate be machined?
Flatness depends on plate size and thickness. Medium plates commonly reach a few hundredths of a millimeter over their length when machined from stress-relieved stock with relaxed finishing. Tell us the flatness callout on your drawing and we will confirm whether it is achievable before quoting.
Is hard anodize worth it on a fixture plate?
For plates that see repeated part loading, clamping or sliding, yes. Type III hard anodizing creates a thick, very hard surface that resists scratching and wear far better than bare aluminum or Type II anodize. It is less important for plates used mainly as static bases.
How do I get a quote for cnc milled 7075 aluminum fixture plate?
Send a 3D model (STEP or IGES) and a 2D drawing with tolerances, material, finish and quantity through the quote form or by email. An engineer replies within 24 hours on business days with price, lead time and any DFM suggestions.
Request a quote
Quote this part
Attach drawings or send several parts at once from the full quote form.
- Emailinquiry@machined-parts-factory.com
- WhatsApp+86 176 2154 1688
- Phone+86 176 2154 1688
- HoursMon–Sat, 08:30–18:00 China Standard Time (UTC+8)