CNC Machined Aluminum Pneumatic Cylinder End Caps
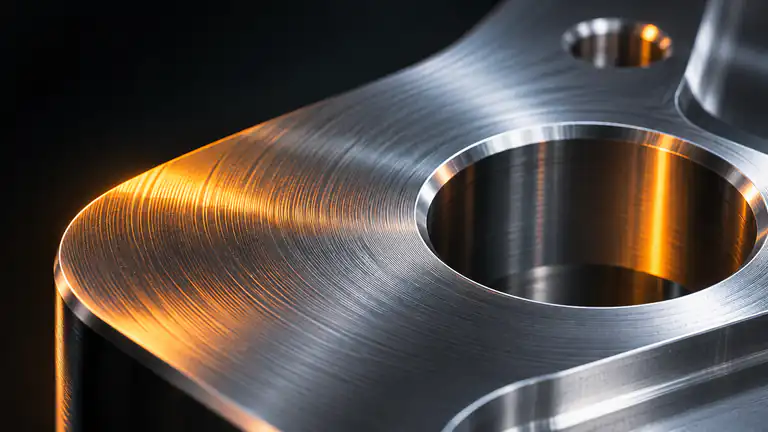
These are custom end caps, heads and rod-end covers for pneumatic and light hydraulic cylinders, CNC machined from 6061 or 6063 aluminum. Air ports, cushion bores, rod-seal grooves and tie-rod holes are cut to 0.01–0.05 mm, and parts are anodized or painted. They are for automation equipment builders and cylinder makers who need non-standard bores or port layouts.
- Material
- Aluminum
- Tolerance
- to ±0.005 mm
- MOQ
- 1 piece
- Prototype lead time
- 3–7 days
- Spigot, rod bore and grooves in one setup
- Hard anodize for wear on seal surfaces
- Ports and cushion holes drilled cleanly
- Leak testing of samples on request
Item ref. 1601003087153 ·
| Process | CNC milling and CNC turning |
|---|---|
| Materials | Aluminum 6061-T6, 6063 |
| Tolerance | 0.01–0.05 mm on critical features |
| Surface Finish | Type II anodizing, Type III hard anodizing, painting, plating, polishing |
| MOQ | 1 piece |
| Drawing Formats | STEP, IGES, X_T, STL, DWG, DXF, PDF |
| Lead Time | Prototypes ~3–7 working days; production typically 10–20 working days |
| Inspection | First-article + 100% critical-dimension inspection; CMM report on request |
Manufacturing
How we make this part
Process, material options and inspection for cnc machined aluminum pneumatic cylinder end caps.
End caps combine a precise spigot that locates the barrel, seal grooves, a rod bore and threaded ports. We machine the spigot, rod bore and seal grooves in one setup so the piston rod runs concentric to the barrel. Ports are drilled and tapped from the side, and cushion-needle holes are drilled to intersect cleanly with internal passages. Tie-rod holes are positioned on CMM-checked patterns.
6061-T6 is strong and machines cleanly; 6063 is common where square cylinder profiles are extruded. Type III hard anodizing, typically 25–75 µm, resists wear on rod-bore and seal surfaces and protects against corrosion from moist compressed air. Clear or black Type II anodizing is used for cosmetic parts. Painting suits colored housings on larger industrial cylinders.
Seal-groove dimensions and surface finish are measured at first article, and ports are gauged. Assembled samples can be leak-tested at your working pressure. Critical dimensions are 100% inspected. Typical uses include compact cylinders, guided cylinders, rotary actuator covers, gripper bodies and custom air-cylinder repairs. Repeat orders run from the same approved program.
FAQ
Frequently asked questions
Why are cylinder end caps hard anodized?
Hard anodizing creates a thick, very hard surface that resists wear from rod and seal motion and protects against moisture in compressed air. It extends seal life and keeps bores from scoring. For static caps with no sliding surfaces, Type II anodize is usually enough.
Can you machine end caps for a non-standard bore size?
Yes. Because the parts are machined, any bore, port size or tie-rod pattern can be produced from your drawing. Tell us the bore, stroke cushioning requirement, port thread and seal types, and we will check the groove dimensions with you.
How do I get a quote for cnc machined aluminum pneumatic cylinder end caps?
Send a 3D model (STEP or IGES) and a 2D drawing with tolerances, material, finish and quantity through the quote form or by email. An engineer replies within 24 hours on business days with price, lead time and any DFM suggestions.
Request a quote
Quote this part
Attach drawings or send several parts at once from the full quote form.
- Emailinquiry@machined-parts-factory.com
- WhatsApp+86 176 2154 1688
- Phone+86 176 2154 1688
- HoursMon–Sat, 08:30–18:00 China Standard Time (UTC+8)